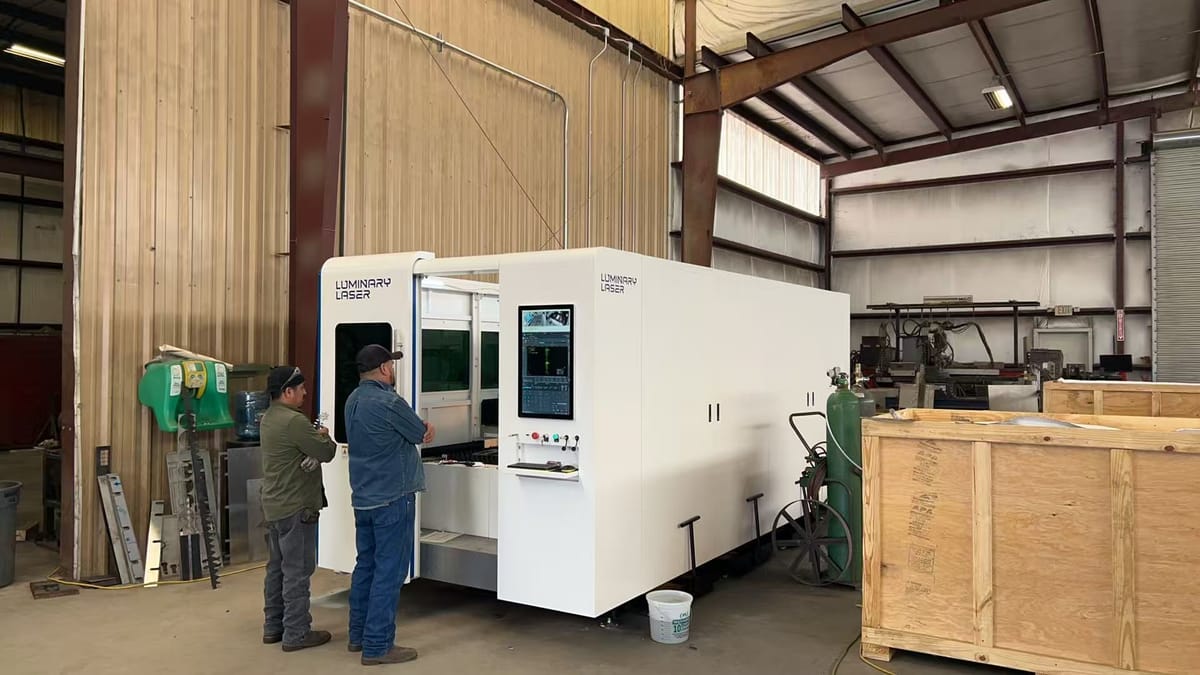
Is fiber laser or plasma better for a fabrication shop?
Neither process is universally better. Fiber laser is commonly evaluated when a shop prioritizes fine detail, small features, controlled edge quality, repeatable automation, and a broad mix of sheet-metal work. Plasma remains a practical process for electrically conductive material when the job mix, plate condition, thickness range, required tolerance, and downstream work support it.
Do not select a process from a single crossover-thickness claim. Published thresholds vary with material grade, source power, plasma system, consumables, assist gas, motion system, cut strategy, and the quality level the buyer accepts. A defensible decision starts with representative drawings and timed sample parts from the work your shop expects to run.
Fiber laser and plasma: practical buying comparison
| Decision factor | Fiber laser | Plasma |
|---|---|---|
| Best comparison basis | Detailed sheet parts, edge requirements, automation, and downstream savings | Conductive plate work, accepted cut standard, rugged material mix, and existing workflow |
| Material scope | Commonly evaluated for carbon steel, stainless steel, aluminum, and other supported metals | Electrically conductive metals |
| Quality decision | Validate holes, slots, corners, edge consistency, and tolerance on real parts | Validate taper, slag, holes, edge condition, and required cleanup on real parts |
| Cost decision | Include assist gas, electricity, optics and service, automation, labor, and secondary work | Include electricity, gas, electrodes and nozzles, labor, cleanup, and secondary work |
| Evidence to request | Timed common nest, process inputs, accepted-part count, and sample inspection | Timed common nest, consumable condition, accepted-part count, and sample inspection |
Start with material, surface condition, and part geometry
List the actual material mix before comparing equipment. Include carbon steel, stainless steel, aluminum, and any coated, rusty, painted, or mill-scale plate that appears in normal production. Plasma is limited to electrically conductive material. Fiber laser process stability and cut quality also depend on material chemistry, surface condition, thickness, and the selected assist gas.
Geometry can be more important than nominal thickness. Record the smallest hole, narrowest slot, tightest internal radius, longest contour, tolerance, edge requirement, and whether parts go directly to forming or welding. A shop cutting simple structural profiles has a different decision than one nesting many detailed sheet-metal parts on a 5 x 10 ft (1.5 x 3.0 m) sheet.
Compare finished parts, not cutting-head speed
Headline traverse or cutting-speed figures do not describe completed throughput. Loading, probing, piercing, corner behavior, nesting, unloading, sorting, slag removal, deburring, rework, and part identification all affect how many acceptable parts leave the cell during a shift.
Build the comparison around a common nest and a common quality standard. Time the process from material presentation through a finished batch, then record accepted parts, operator attention, consumables, gas use, secondary work, and interruptions. This prevents a fast segment of the cycle from being mistaken for lower total production cost.
Use your real thickness distribution
A shop should compare the percentage of annual work at each material and thickness, not only the thickest plate it may occasionally cut. For example, separate recurring 0.125 in (3.2 mm), 0.5 in (12.7 mm), and 1.0 in (25.4 mm) work instead of treating all three as one average job. Add expected batch size, annual part quantity, and schedule pressure for each group.
If most revenue comes from thinner, detailed parts, the preferred process may differ from a shop dominated by heavy, simple profiles. When the mix is genuinely split, the correct answer may be process specialization, retained plasma capacity alongside a laser, or a staged investment rather than forcing every job through one machine.
Calculate total operating cost with shop-specific inputs
A useful cost model includes equipment financing or depreciation, electricity, assist gas or plasma gas, compressed air, consumables, preventive maintenance, planned service, operator labor, loading and unloading labor, scrap, secondary finishing, and facility requirements. Use supplier utility specifications and your local rates instead of a universal cost-per-hour claim.
Calculate both cost per scheduled hour and cost per accepted part. A process with a higher hourly input can still be economical when it reduces secondary operations or increases accepted output. The reverse can also be true when an expensive configuration is underutilized or requires inputs that the shop has not planned to supply consistently.
Evaluate automation, staffing, and downstream work
Ask how material will be staged, loaded, nested, unloaded, sorted, and moved to the next operation. A machine should be evaluated as a production cell, not as an isolated cutting source. Available floor space, crane or forklift access, sheet size, scrap handling, fume control, and operator skill all influence the practical configuration.
Downstream labor deserves explicit measurement. If parts require grinding, hole cleanup, edge preparation, identification, or rework before bending and welding, include that time in the comparison. The purchasing team should agree on the acceptable edge and dimensional standard before suppliers produce samples.
Run a controlled sample-cut comparison
Send each supplier the same drawing package, material grade, certified thickness, surface condition, quantity, and acceptance criteria. Include both routine parts and difficult features. Request the process settings used, actual cycle scope, consumables condition, gas type, and any secondary work performed before the samples are presented.
Inspect dimensions, holes, slots, corners, taper, dross or slag, heat effects, edge consistency, part flatness, and readiness for the next operation. Keep the comparison reproducible. Demonstration parts selected by a supplier can show capability, but they do not replace a test based on your production mix.
What to include in a quote request
Provide part drawings, annual quantities, batch sizes, materials, thickness distribution, standard sheet dimensions, tolerance, edge requirements, current secondary operations, and the target shift pattern. State whether sheets are typically 5 x 10 ft (1.5 x 3.0 m), 6.5 x 13.1 ft (2.0 x 4.0 m), or another format.
Also document electrical service, gas availability, compressed-air capability, ventilation or dust-collection planning, delivery access, operator staffing, and installation timing. Final utility and safety requirements must be confirmed from the selected equipment documentation with qualified local professionals and applicable codes.
Technical references
Technical sources and scope.
Supplier-specific performance claims are not treated as universal. Confirm the selected process with controlled sample cutting and the final equipment documentation.
FAQs
Frequently asked questions.
Is fiber laser better than plasma cutting?
Not for every job. Fiber laser is often evaluated for detailed, automated sheet-metal production, while plasma remains practical for conductive plate work where its cut standard and workflow meet the shop's requirements. Compare accepted parts and total production cost using your own drawings.
Which process is better for thick plate?
There is no responsible universal thickness cutoff. Material, power, plasma configuration, edge requirement, tolerance, gas, consumables, and secondary work change the answer. Test representative thick parts and compare the complete process under the same acceptance criteria.
Which has the lower operating cost, fiber laser or plasma?
Operating cost depends on local electricity and gas rates, consumables, maintenance, utilization, labor, accepted throughput, and secondary operations. Calculate cost per accepted part with supplier utility data and your shop's actual rates rather than relying on a generic hourly figure.
What should be included in a fiber laser versus plasma sample test?
Use identical drawings, material grade, thickness, surface condition, quantity, and quality criteria. Record the full cycle scope, process inputs, operator work, accepted parts, edge condition, dimensions, consumables, and any cleanup required before the next operation.